HPVR1000 Combination Truck: The Ultimate Vacuum Truck for Mining Operations
The HPVR1000 Combination Truck is engineered to meet the rigorous demands of mining operations, where durability, efficiency, and safety are paramount. Built to thrive in the harshest environments, this vacuum truck is equipped with the iconic HPLR 1200 liquid ring pump, a powerful and reliable component designed by Highpoint Manufacturing. This advanced pump system ensures continuous heavy-duty operations without the risk of overheating, thanks to its integrated water-cooling system.
Unlike its counterpart, the HPVR500 Combination Truck, which excels in municipal tasks, the HPVR1000 Combination Truck is tailored for the unique challenges of the mining industry. It features larger suction booms and additional locking clamps, providing enhanced capability to manage the demanding tasks of clearing blocks, removing sludge, and maintaining mine infrastructure. These features, combined with the truck’s robust design, make it an indispensable asset in any mining operation.
Safety is at the forefront of the HPVR1000 Combination Truck’s design, fully complying with stringent mining safety regulations. The truck’s construction ensures that it can handle hazardous materials and conditions with ease, providing peace of mind to operators and management alike. The HPVR1000 Combination Truck is not just a tool but a long-term investment in the efficiency and safety of your mining operations.
Choosing the HPVR1000 Combination Truck means investing in a solution designed specifically for the mining sector. With superior engineering, compliance with industry regulations, and advanced features, the HPVR1000 Combination Truck stands out as the ultimate choice for industrial vacuum and combination trucks in mining. Explore the HPVR1000 Combination Truck and experience the difference in quality, performance, and reliability tailored for the most challenging environments.


Request A Quote
The Vacuum Pump System
The HPVR-1000 Combi, equipped with a robust Vacuum pump, ensures reliable performance and long life. Featuring advanced overheating protection, this low-maintenance pump operates quietly and efficiently, delivering a flow rate of 4150 m³/h at 0% vacuum. A stainless steel mesh strainer safeguards the pump, while a one-way valve guarantees uni-directional flow.

The Jetting System
The HPVR-1000 Combi is equipped with a High Pressure Pump, protected by dual anjet filters to prevent small particles from entering. Enhanced safety features include a pressure relief valve and a pneumatic-actuated shut-off valve for the pump supply line. The pump, capable of 290 l/min at 200 bar, is connected to a three-position pneumatic valve allowing water to flow back into the tank during nozzle changes, ensuring efficient operation and water conservation.

The Hose Reel
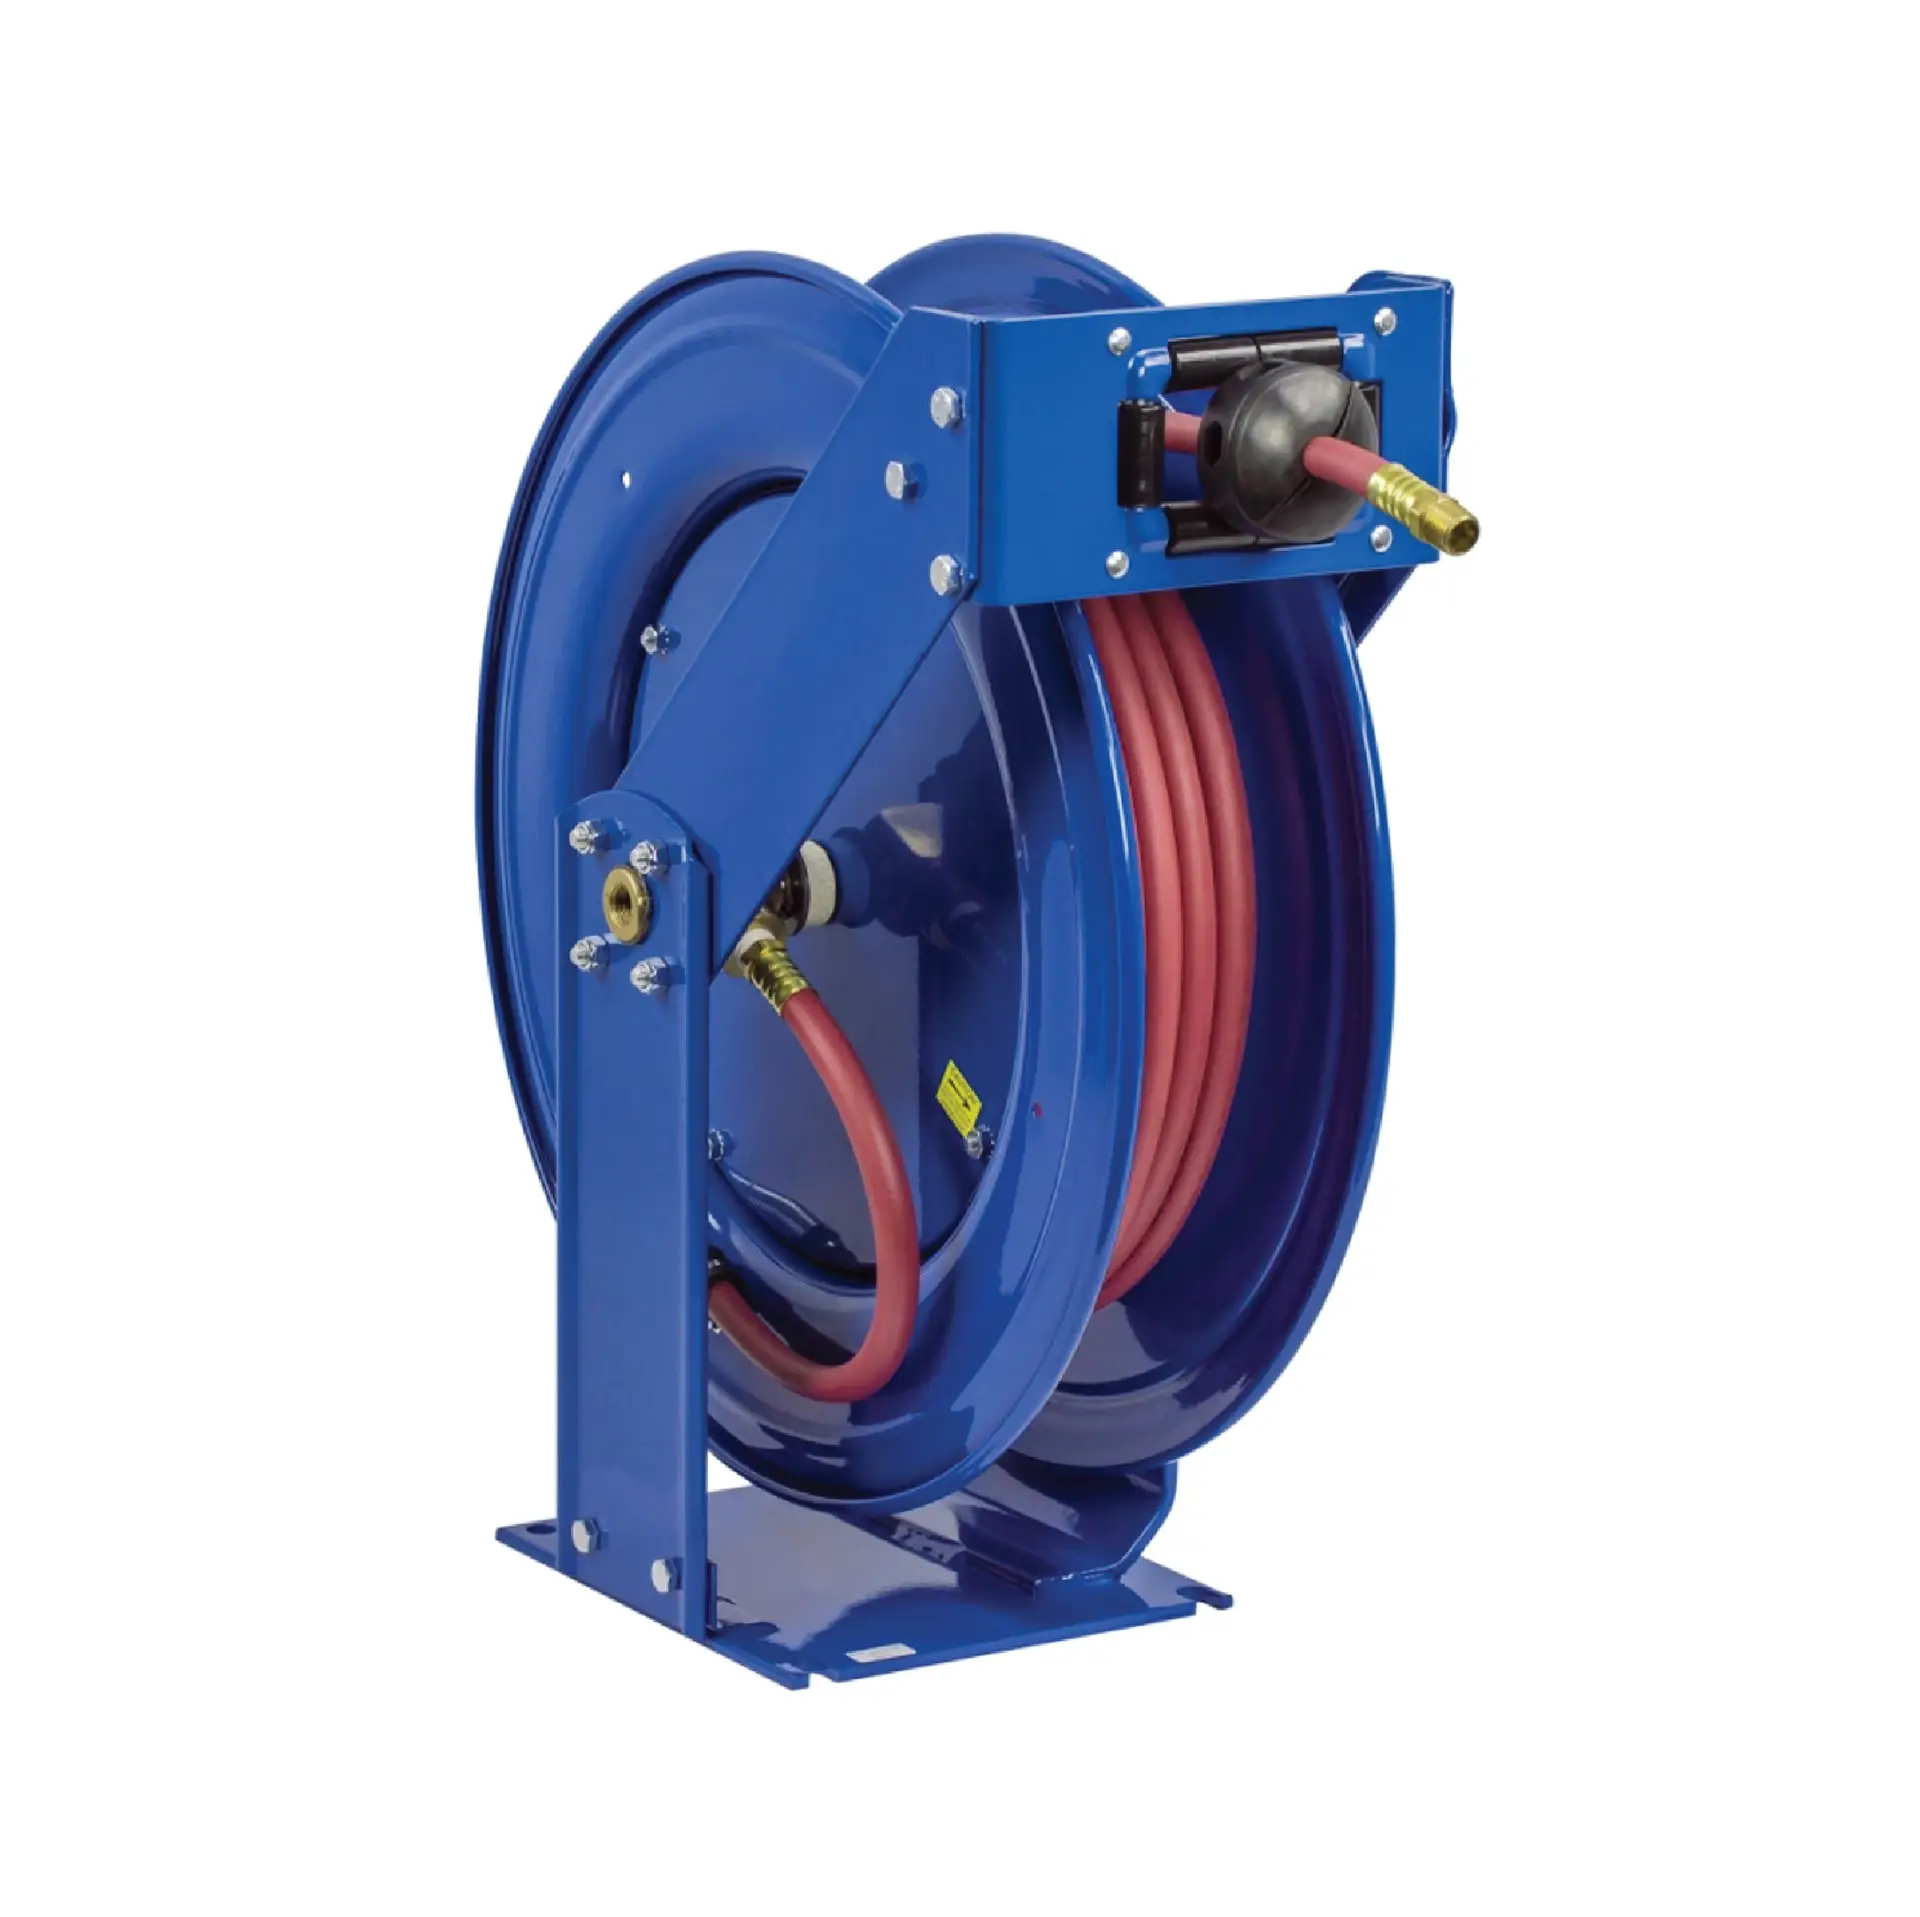
The HPVR1000-combi features a state-of-the-art hose reel at the rear, fully operated hydraulically for winding, unwinding, and swinging open and closing. It comes standard with a 120m long 1″ jetting hose and includes a work light to illuminate the work area.
The control panel, conveniently placed on the hose reel, is simplified to reduce operator error and includes a fast-acting emergency stop button.

Vacuum Pump Water Reservoir
The HPVR1000-Combi features a robust 2,000L water reservoir, purpose-built to support the vacuum pump and ensure seamless operation of the liquid ring pump system. This large-capacity reservoir not only provides sufficient water for effective cooling but also enables operators to maintain continuous workflow without interruption. Enhancing efficiency further, the system is designed to recycle the water used during operation, directing it back into the tank to minimize waste and reduce water consumption.

-
ENZ Grenade Bomb Nozzle
R25,060.00 -
ENZ Retrojet Nozzle
R9,330.00